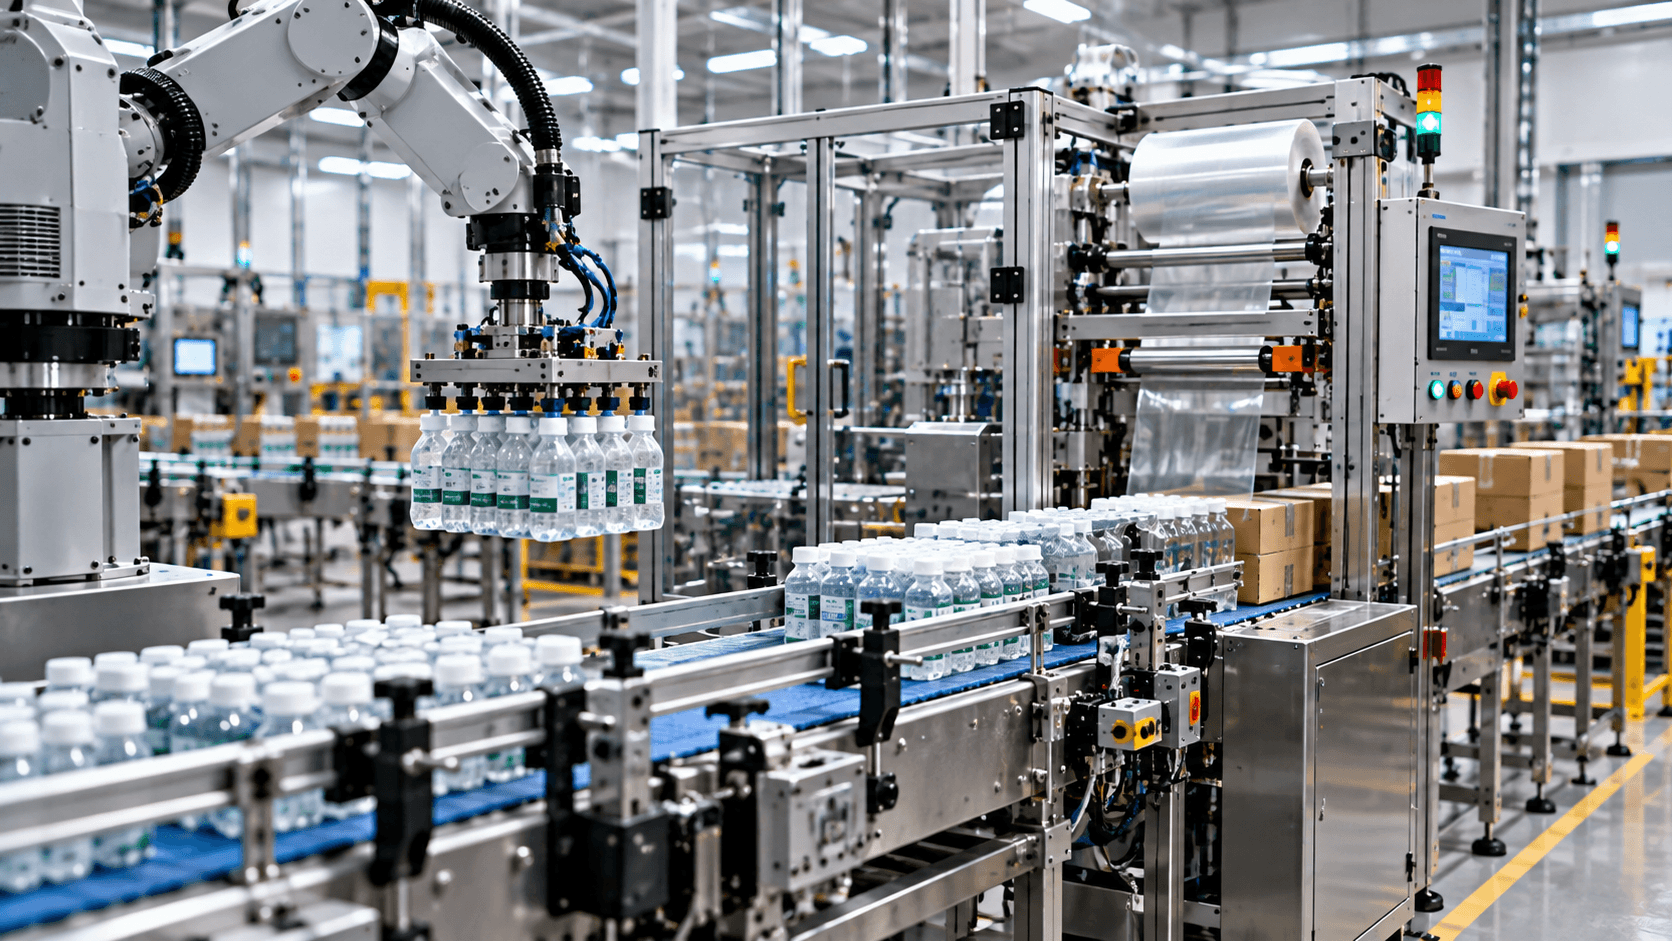
High-Speed Production Demands
Extreme speeds make manual inspection and monitoring difficult
Intelligent Automation for High-Speed, High-Volume FMCG Manufacturing
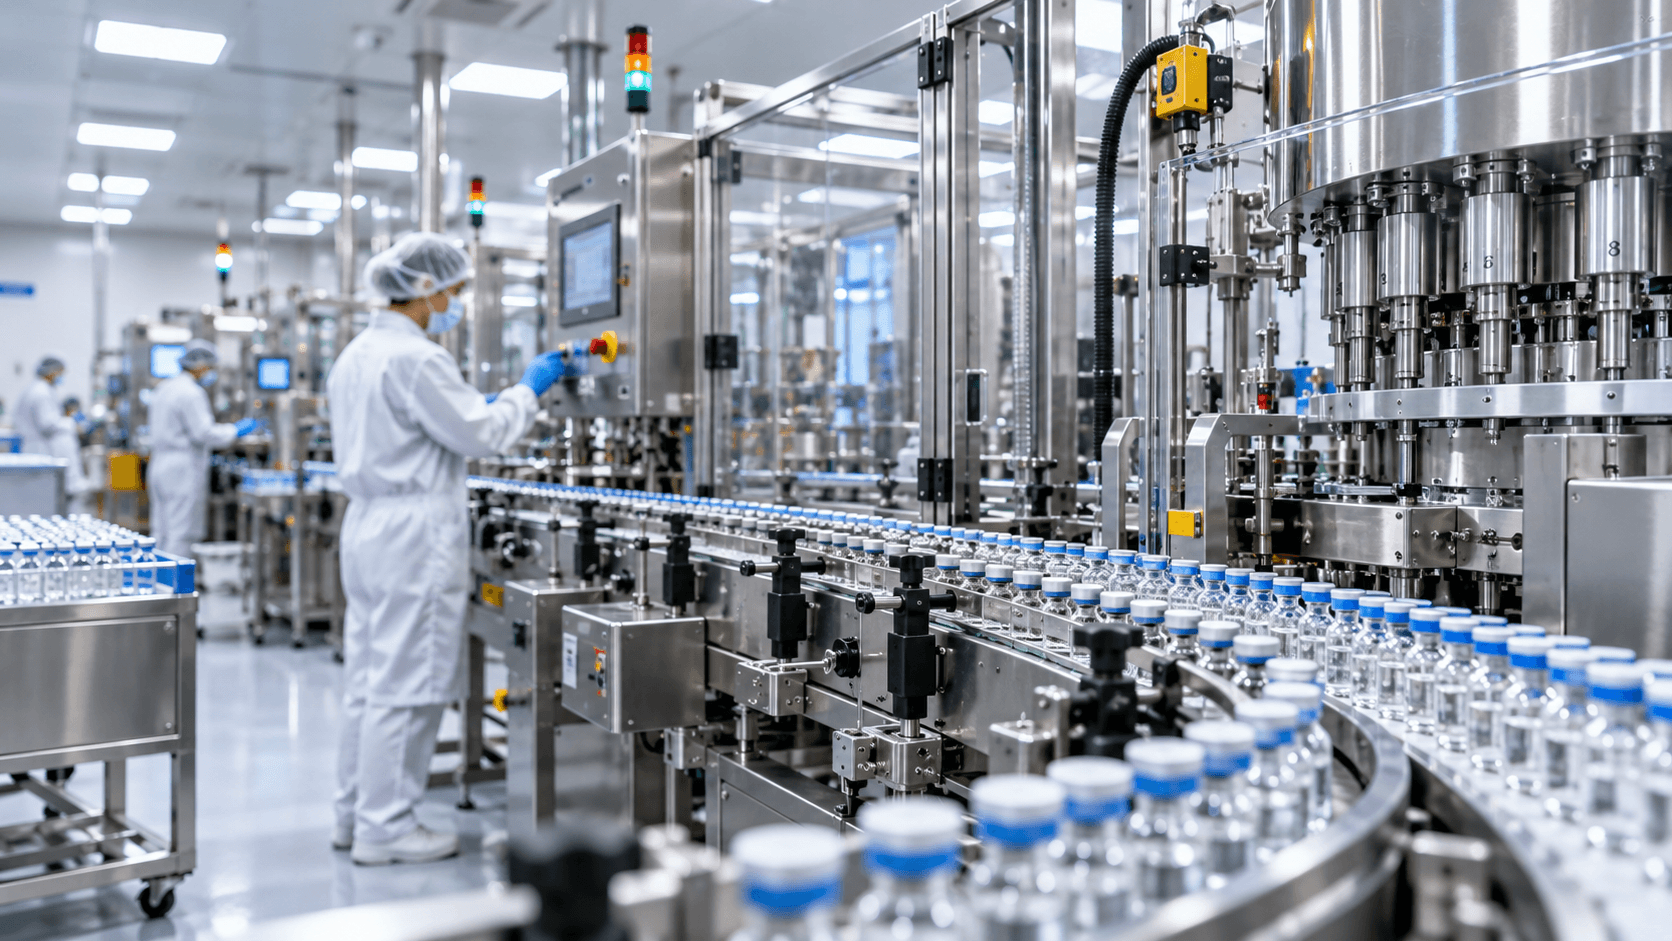
Vis-Con Automation delivers FMCG Automation Solutions that automate production processes, improve inspection accuracy, reduce downtime, and optimize manufacturing performance. Expertise includes FMCG Manufacturing Automation, FMCG Process Automation, Packaging Automation, AI-powered vision inspection, SCADA systems, and production line integration.
Vis-Con Automation delivers FMCG Automation Solutions that automate production processes, improve inspection accuracy, reduce downtime, and optimize manufacturing performance. Expertise includes FMCG Manufacturing Automation, FMCG Process Automation, Packaging Automation, AI-powered vision inspection, SCADA systems, and production line integration.
FMCG · engineered, validated, supported
Every architecture we hand over in this sector is built to satisfy the standards below from day one — not retrofitted to them later.
Complete FMCG Production Line Automation
Food & Beverage Manufacturing
Personal Care & Home Care Manufacturing
High-Speed Packaging Operations
Product Quality Inspection
Production Monitoring & Analytics
Warehouse & Material Handling Integration
The recurring constraints we are called in to remove — and the reason most of these plants automate in the first place.
Extreme speeds make manual inspection and monitoring difficult
Filling, labeling, packaging, coding variations impact brand
Equipment failures and manual interventions reduce throughput
Disconnected machines and isolated data hinder decisions
Barcode verification, batch tracking, labeling, production records
Coordination of equipment, conveyors, packaging, inspection, software
Each pain point maps to an engineered capability you can open and read in full.
Talk to a Vis-Con automation engineer about your facility, its constraints and the compliance you need to satisfy.
VIS-CON AUTOMATION — INDUSTRIAL SYSTEM INTEGRATOR
GANDHINAGAR, GUJARAT · PAN-INDIA DELIVERY